← Semiconductors 101: a free course following the life of a chip
Semiconductors 101, unit 18
Control charts and daily monitoring
A measured number only means something next to a yardstick that says whether the process is still behaving as usual. The control chart is that yardstick: it shows a process changing before anything has been made wrong.
Goals
- Explain where control limits come from and how they differ from spec limits, and tell OOC from OOS.
- Explain why a fab may stop and look for a cause even when everything is within spec, and even when no point is outside the limits.
- Say what monitor wafers, FDC and APC each look at and when, and why a system correcting every lot by rules does not clash with "leave it alone inside the limits".

Step by step
- Calculate the control limits from the process's own data from a stable period, and plot one point per lot measured: outside the control limits is OOC, outside the spec is OOS.
WhyThis yardstick says "this is what this step on this tool normally looks like" and has nothing to do with what the customer wants; when a process wobbles only a little, OOC often comes before OOS.
If notWait for OOS to act and things are already bad; every lot the tool ran since the last normal measurement may be affected too and has to be tracked down.
- Even with no point outside, check whether 8 points in a row sit on the same side of the center line.
WhyIf the process hasn't changed and the numbers wobble evenly, each point is about as likely to land above as below; 8 in a row below the line has a chance of 1 in 256, and 8 above is just as rare.
If notA part slowly wearing or a chemical slowly used up keeps every point inside the limits; wait for one to cross and it is caught late.
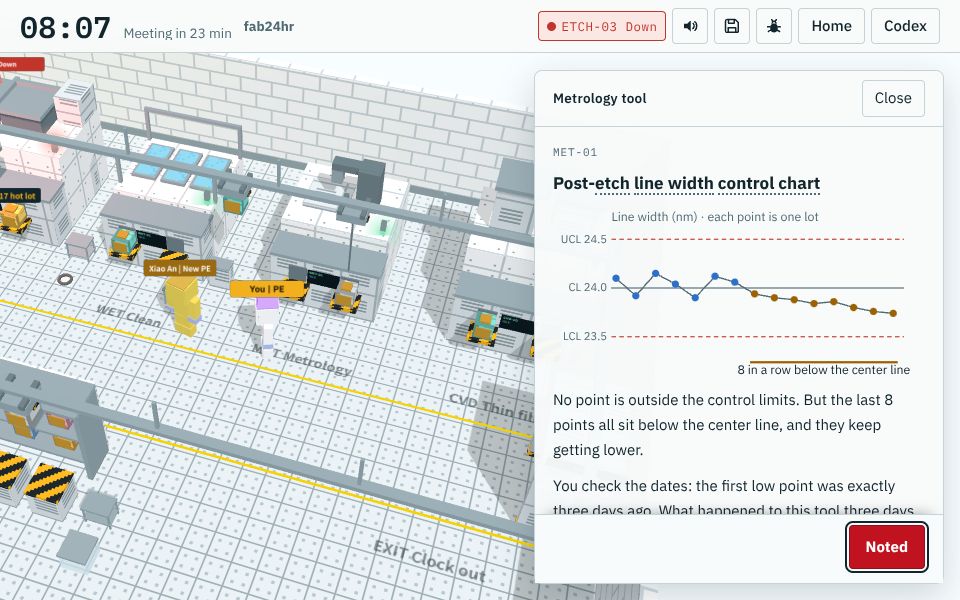
A screen from the game fab24hr; the tools, lot numbers and people are fictional. Play this part in the game → - Leave small ups and downs inside the limits alone; don't adjust the tool on the spot.
WhyThat is natural wobble, many small causes added up, and it is how the process normally behaves. Correction from measurements is something else: when overlay is off, for example, the system shifts the scanner's position a little for the next lot, by a calculation designed in advance.
If notAdjust by hand at every small shift and the process only wobbles more.
- Before production or on a schedule, run a monitor wafer that won't ship, plot its number on the control chart, and let product in only when it's inside the limits.
WhyProduct is covered in patterns and hard to measure, some measurements ruin the wafer, and by the time product is measured several lots may have gone through.
If notThe tool drifts and nobody knows, the next customer lot goes straight in, and the whole lot comes out wrong.
- As the tool runs each wafer, have FDC compare the curves its sensors record with what this step normally looks like, and call someone when one crosses its threshold.
WhyMeasurement waits until the wafers are done and takes only a few, and a monitor wafer comes only every so often; FDC looks at every wafer and sees a tool acting strange while the work is happening.
If notWhen a tool goes wrong between two measurements, its sensor readings quietly go out of range with nobody watching, and by the time measurement catches it several lots have gone by.
- After a repair or maintenance, leak-check if the chamber was opened, run a few dummy wafers that won't ship to settle the chamber (season), then do the qual run; only when it passes does the tool take product.
WhyPutting it back together doesn't make it the same as before, and the maintenance itself can go wrong.
If notThe first few wafers after a chamber is cleaned come out different from usual; take product straight away and the ones that come out off are the customer's.
- To change any process condition, go through change control first: write down what will change and why, assess the impact, try it on a small scale, change it only after the right people have reviewed and signed, and keep the record; after the change, watch the first few lots on the control chart more closely.
WhyA small difference in a number can make a small difference in the product, and sometimes it only shows up when the wafer is finished and its electrical numbers are measured; and what customers qualified is the original way of making it.
If notWithout a record, after a problem there is no way to trace which change it was or from which lot it started; a person changing a set condition on the spot is a change that skipped the procedure, even if the result looks fine.
Key ideas
Control limits are the process's own "normal"; spec limits decide whether it can be used
Each time a lot is measured, post-etch line width for example, a point goes on the control chart, in time order from left to right. The center line is the usual average; the upper and lower control limits are usually drawn three standard deviations above and below it, the standard deviation being a yardstick for "how much it normally wobbles". When the process hasn't changed and the numbers fall in a bell shape, fewer than three points in a thousand land outside. These lines are calculated from the process's own data while it was stable, and have nothing to do with what the customer wants; the range the customer or the design requires is the spec limits. Outside the control limits is OOC (out of control), which says "this is not normal anymore"; outside the spec limits is OOS (out of spec). When a process normally wobbles only a little, its control limits sit inside the spec limits, so OOC often shows up before OOS: the process is seen changing before anything has gone bad. The other way round, if the numbers normally wobble past the spec limits, every point can be "normal" and the product still fails; then it is the process itself that has to change.
No point outside, yet 8 in a row on one side counts too
If the process hasn't changed and the numbers wobble evenly up and down, each point is about as likely to land above the center line as below it, like a coin toss; tails 8 times in a row has a chance of 1 in 256. So 8 points in a row below the center line more likely means something has changed. The rule is often written as "several points in a row on the same side of the center line" (8 is common), catching things like a part slowly wearing or a chemical slowly used up. Every point is still inside the limits, but the whole string keeps heading one way. Wait until it crosses the limits, or the spec, and every lot made in the meantime has to be tracked down. The more rules a fab uses, the earlier it catches things and the more false alarms it gets; each fab sets its own.
Don't chase the wobble by hand; the system corrects by rules: feedback and feedforward
Tools drift slowly: deposits build up on an etch chamber's walls, a polishing pad gets smoother with use, and the same settings give results that creep off bit by bit. The drift between two rounds of maintenance is often left to a system that corrects each lot a little by fixed rules, called APC (advanced process control). Feedback looks at the tool's own latest measured results and corrects the next lot; feedforward looks at a number measured at the step before and adjusts this lot before it runs: if a film came out a little thick, for example, the polishing step after it (CMP) polishes a little longer. This doesn't clash with "leave small wobbles inside the limits alone"; the difference is how you adjust. A person who sees one point a little off and adjusts by hand by the full amount is mostly reacting to noise, and adds the wobble in a second time. APC feedback moves only the few numbers agreed in advance, averages several lots and moves only a little each time, so it follows slow drift in one direction; feedforward handles "what's coming in is different". A sudden big jump is still flagged by the control chart, and people stop to find the cause.
Tools prove themselves too: monitor wafers on a schedule, FDC on every wafer
A monitor wafer (also called a control wafer) is the fab's own wafer that never ships, usually a blank wafer with no pattern, which is flat and easy to measure (for measuring how much is etched or polished off, it first gets a film). Before customer wafers go into a tool, or at a set interval, one is run with the usual settings and measured (how thick a film grew, how much was etched off, or how many particles were added), and the number goes onto this tool's own control chart: product goes in only when it is inside the limits, and when it is outside or keeps heading one way, the OCAP says to stop the tool first. After maintenance, too, a few wafers that won't ship are run first to settle the chamber (season), then a monitor wafer for the qual run. But measurement waits until the wafers are done and takes only a few, and a monitor wafer comes only every so often, so between two of them a tool may already have run several lots. That is why, as the tool runs each wafer, its sensors keep recording pressure, temperature, power and gas flow, and FDC (fault detection and classification) compares those curves with what this step normally looks like; when one crosses its threshold, it sends an alert to call someone, then sorts out what kind of problem it is: a part that really broke or wore down, or a sensor that just cut out for a moment. The tool also reports by itself: a mild warning usually lets it keep running with the yellow light on; a serious alarm usually stops it, with the red light on.
Common misconceptions
- People sayAs long as it's within spec, there's no problem.
- In factNot necessarily. OOC often shows up before anything fails: the product is still usable, but the process has changed, like arriving on time yet far slower than usual. A common first step is to put the lot on hold and measure again, to rule out a drifting metrology tool, then follow the procedure written in advance (the OCAP) to find the cause; in the end an engineer decides whether the lot goes on to the next step or stays held for more checks.
- People sayAdjusting the tool the moment a point moves a little is the safest choice.
- In factEvery process has a natural wobble made of many small causes, and that is simply what it looks like. Treat that wobble as a problem and adjust the tool every time a point moves, and the process wobbles more, not less. The other half of a control chart's job is telling you when not to act: leave the up-and-down inside the limits alone, and look for a cause only when points cross the limits or line up in one direction.
Read
- What is an SPC control chart, and how are OOC and OOS different?
- What are monitor wafers and dummy wafers, and how does a fab tool prove it's still OK?
- What is APC? How a chip fab corrects itself after measuring: feedback and feedforward
- What is FDC? How a chip fab keeps watch on its tools' sensors
Further
- What is PM (preventive maintenance), and why do fab tools stop on a schedule?
- What is change control in a chip fab, and why does one change need so many sign-offs?
Play
Think
- The control chart says "still within spec, but no longer normal", and the lot is waiting. If it goes on to the next step, who pays? If it stays held, who pays?
- Control chart rules and FDC thresholds catch problems earlier the tighter they are, and raise more false alarms too; set them too loose and slow decline goes unseen. If you were setting them, where would you draw the line? Will someone called out by false alarms many times still look carefully next time?
Teaching materials: slides
The key ideas, diagram, machines and questions of this unit as a slide deck, ready to project or to put into your own handouts.
Download slides (PPTX)186 KBDownload slides (PDF)198 KB
Free to use in class and for non-commercial teaching. Please credit fab24hr. Do not sell it or present it as your own work. Spot a mistake? Report it
Cite this article"Semiconductors 101, unit 18:Control charts and daily monitoring" fab24hr, updated . https://fab24hr.com/en/learn/spc/